Promotional Cartons That Had to Look Clean on Shelf
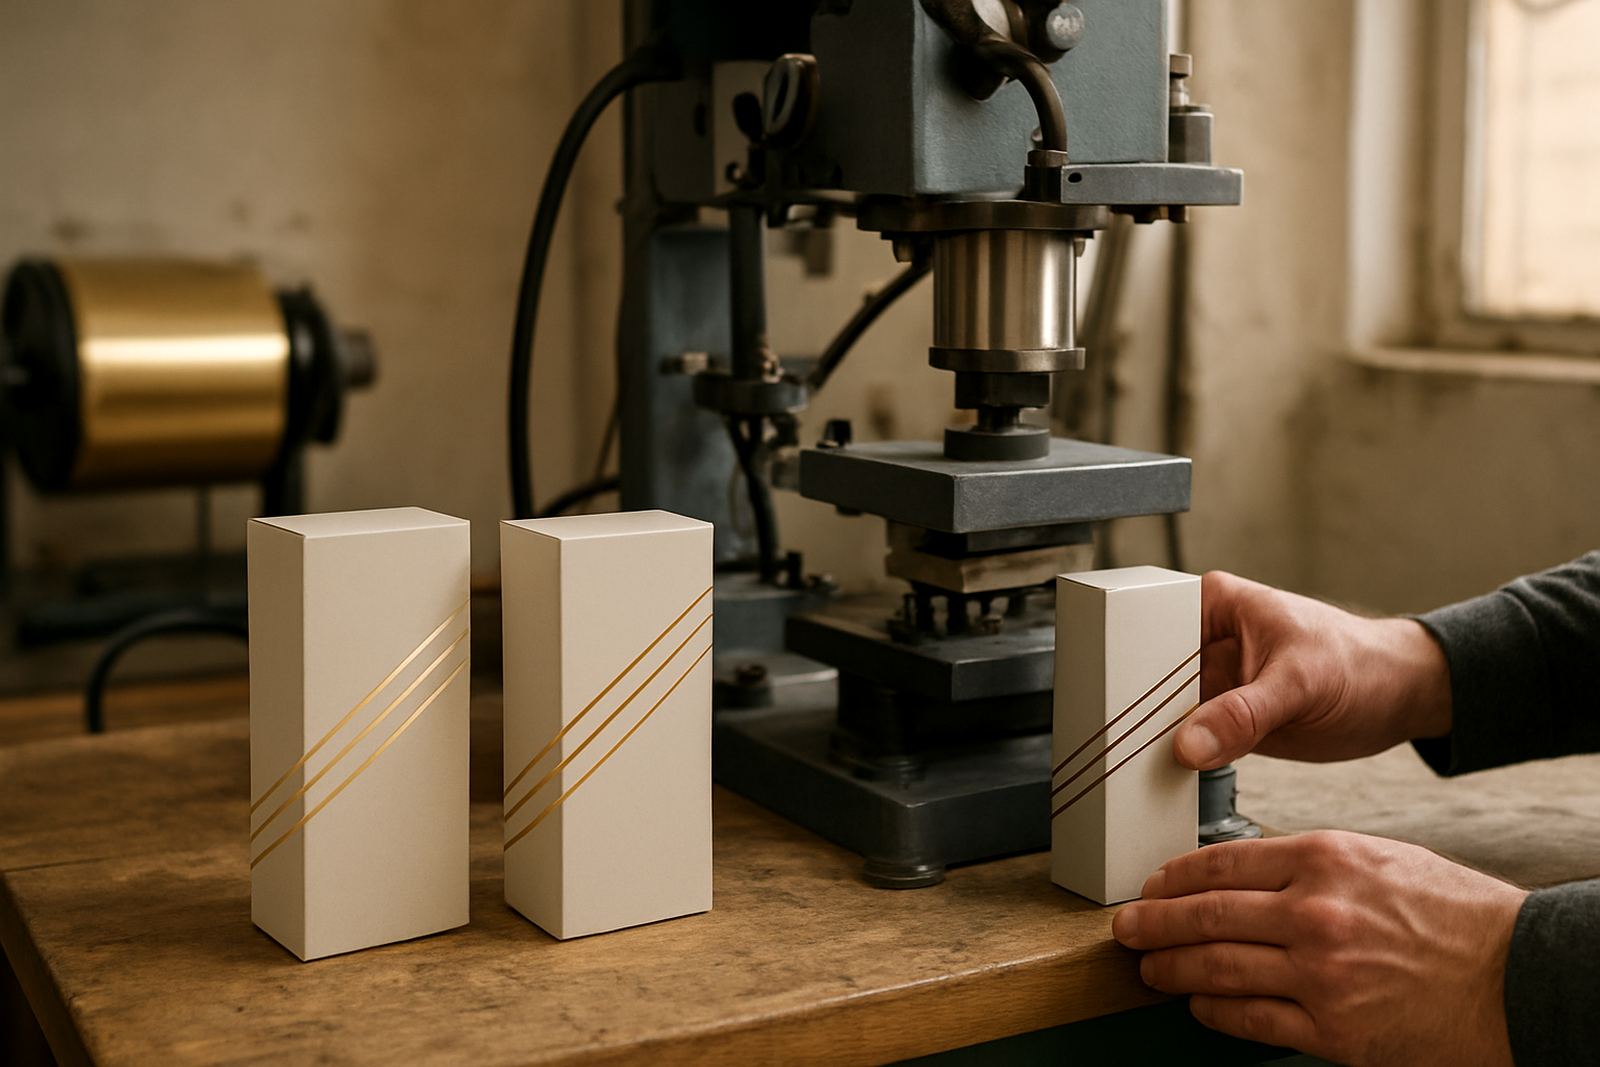
The job came from a contract packer in Midrand that was handling a cosmetic carton promotion batch for a client in Gauteng. The cartons had to carry a bright foil mark on the front panel, with clean edges, no scuffing and a consistent finish across the full run. In this type of work, the carton is often the first thing a buyer sees, so the foil needed to be sharp even on short notice.
The brief was simple to say and hard to execute. The press had to suit lightweight carton board, keep registration steady from the first sheet to the last, and run without constant adjustment while the packing line was already busy. The team also wanted a setup that their operators could repeat for future promotional work, not a one-off fix that only worked on the day.
- Client type: contract packer
- Town: Midrand
- Application: cosmetic carton promotional batch
- Finish required: clean hot-foil marking on printed cartons
What Made the Run Tricky in Midrand
The main constraint was timing. The cartons were due for dispatch within a short production window and the packer could not afford a long setup or trial-and-error with pressure and heat. There was also the usual Johannesburg practical issue of power stability, so the machine had to be checked carefully before the run started. On carton work, a small temperature drift can show up fast as light patching or fuzzy edges.
The board stock was another factor. Cosmetic cartons are often thin enough to show pressure marks if the tooling is too aggressive, but still need enough heat to take a bright foil impression. Midrand production spaces can also be tight, so the press had to be positioned with enough clearance for operator movement and safe loading. We kept the setup compact and made sure the working height suited the team on shift.
- Short turnaround required
- Light carton board needed controlled pressure
- Power stability checks done before production
- Operator access planned for a busy packing floor
The Press Setup We Supplied and Commissioned
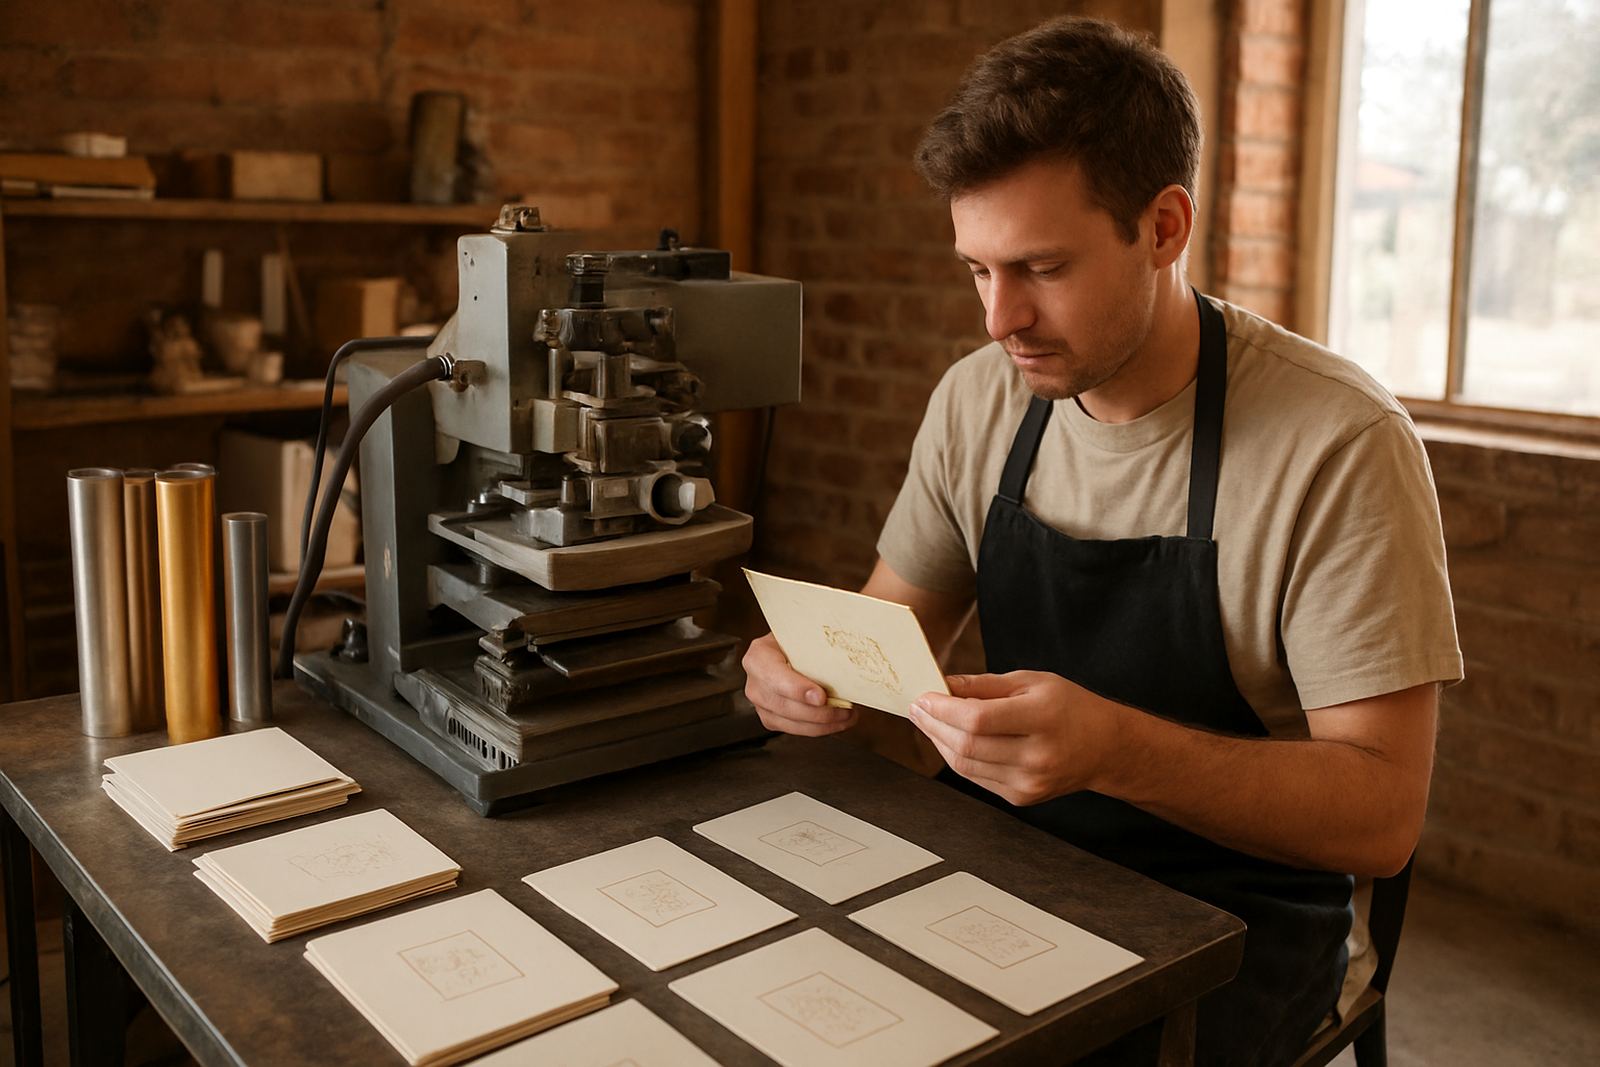
We supplied a pneumatic hot-foil stamping press suited to short and medium carton runs, with a heated platen, adjustable dwell time and stable pressure control. The unit was configured for repeatable impression depth and fine positioning, which matters when a carton has a small logo or a narrow foil line close to a crease. We also supplied the foil grade most suited to cosmetic packaging, where colour clarity and edge definition matter more than heavy coverage.
Our technical team handled installation, checked the heater calibration and set the pressure to match the carton board. We then mounted the die, tested alignment and ran sample impressions until the foil held properly without over-crushing the substrate. Once the press was stable, we handed over a clear operating sequence so the team could keep the settings consistent through the full batch.
- Pneumatic press for controlled repeat runs
- Heated platen with adjustable temperature
- Pressure and dwell set for carton board
- Die mounting and foil matching completed on site
- Operator handover included basic setup steps
Three Weeks From First Call to Full Batch
Week 1 was the site assessment and specification check. We reviewed the carton board, print area and expected batch size, then confirmed the press format and foil type. In Week 2 we completed installation, heater calibration and test stamping. That stage included a few small adjustments to pressure and foil feed because the carton surface had a slightly coated finish that needed careful handling.
Week 3 was production support. We stayed close to the run while the operator team finished the promotional batch, checking the first cartons from each shift and watching for any change in impression quality. Once the line was steady, the packer was able to complete the job without stoppages or rework. The whole point was not just to finish the order, but to leave the site with a setup that could be repeated next month if needed.
- Week 1: assessment and specification check
- Week 2: installation, calibration and trial samples
- Week 3: live production support and handover
What the Packer Saw in the Finished Cartons
The batch came out with a clean foil mark, even colour across the run and no visible hot spots around the impression area. More importantly, the cartons stayed flat and presentable after stamping, which helped the packer keep through-put moving without sorting out damaged pieces. The foil finish lifted the presentation of the promotion pack without forcing the client into a slower production method.
For a contract packer, that matters in practical terms. It means fewer rejects, less time on touch-ups and a better chance of meeting retail dispatch dates. The operator team also had a clearer process for future runs, so the same carton format can be set up again with less interruption. On work like this, consistency is worth more than a flashy first sample.
- Sharper impression on the carton face
- Less waste from crushed or marked pieces
- Faster changeover for repeat orders
- Better control for future promotional runs
What We Would Repeat on the Next Cosmetic Run
If we were doing the same project again, we would follow the same basic sequence: check the stock first, match the foil to the print finish, set the pressure conservatively and test for a full shift before releasing the batch. For cosmetic cartons in Midrand and the wider Johannesburg area, that order saves time and avoids the usual frustration of chasing a finish after the line is already committed.
We would also keep the same maintenance approach. Preventive servicing, heater checks and die alignment are small tasks, but they stop bigger problems later. In a busy packaging environment, especially where load-shedding or a stop-start supply can interrupt the day, it helps to have a press that starts cleanly and stays in spec. That is the difference between a press that merely runs and one that can be relied on for contract work.
- Check stock before setup
- Match foil to the printed finish
- Use conservative pressure first
- Keep servicing and calibration on schedule
Key facts
| Project location | Midrand, Gauteng |
|---|---|
| Client type | Contract packer |
| Press type | Pneumatic hot-foil stamping press |
| Application | Cosmetic carton promotional batch |
| Timeline | 3 weeks from first call to production handover |
| Key services | Installation, die mounting, foil matching, calibration, operator training |